Capabilities
Tooled, pressed and ground in our own plants
15 presses from 5 T to 100 T, an in-house tool room, specialised grinding and wire bending. Here is what each one does, the materials we work in, and the capacity we have free.
Press shop
15 presses, 5 T to 100 T
Strip goes in on coil feeders or by hand, through compound dies and progressive dies made in our own tool room.
| Presses | 15 |
|---|---|
| Press force | 5 T to 100 T |
| Feed | Coil feeders, or by hand |
| Dies | Compound dies and progressive dies, made in-house |
| Stock thickness | 0.1 to 5.0 mm |
| Material | Mild steel; carbon spring steel, grade EN 42J or EN 9 (C80 or C55); stainless SS 304 or SS 316 |
| Installed capacity | about 200,000 pcs/day |

Tool room
Our own dies
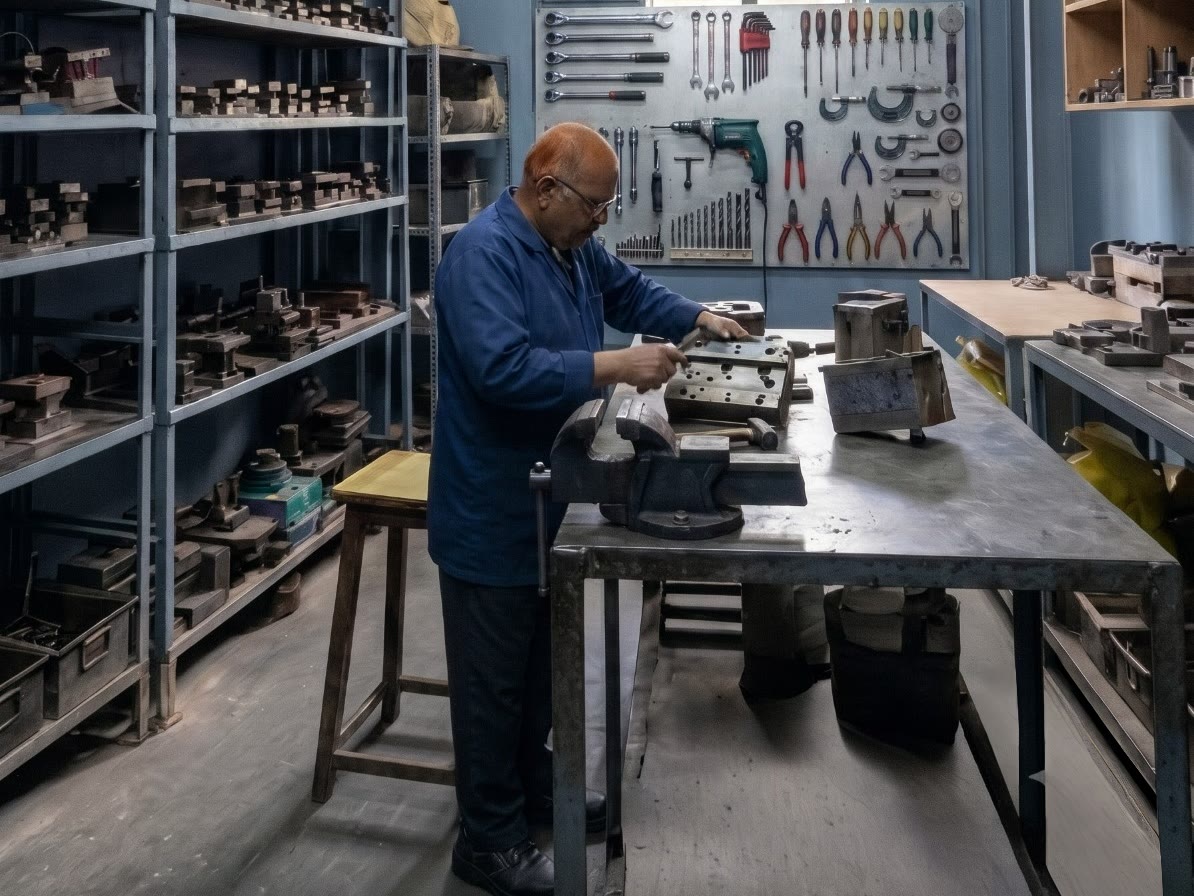
Dies are made and maintained in our own tool room, so a drawing change does not wait on an outside toolmaker.
- Equipment
- Lathe, milling, drilling and wire EDM, all in-house
- New die
- Timeline confirmed once we have studied your drawing
- Die types
- Compound dies and progressive dies
- Tool ownership
- Photoray makes and owns the tooling
Grinding
± 0.005 mm on thickness
Specialised grinding machines, including a rotary grinder. Ground thickness is held to ± 0.005 mm, measured per part at four points on a comparator stand.
± 0.005 mm
Ground thickness
Measured per part at four points on a comparator stand.
Wire bending
Split pins and wire forms
Split pins and customised wire-formed parts, bent in-house.
- Sizes
- Any diameter and length, to your drawing
- Materials
- Mild steel or carbon spring steel wire, or stainless SS 304 or SS 316
Capacity
Room to grow a part with us
Headroom is the number that matters: it tells you whether a part can grow with us without a new vendor and a new approval cycle.
200,000
Installed capacity, pcs/day
Estimated across all 15 presses.
75%
Current utilisation
Share of installed capacity in use today. The other 25% is open for new parts.
50,000
Headroom, pcs/day
Installed capacity minus current output.
Materials
The steels we work in
Every part is made from 0.1 to 5.0 mm stock in one of these grades, or in the grade named on your drawing.
| Material | Grade | Used for |
|---|---|---|
| Carbon spring steel | EN 42J (C80) | Circlips, E-clips, snap rings, conical, wave and star washers, slotted dowel pins |
| Carbon spring steel | EN 9 (C55) | Washers, shims and pressed parts that need strength and some spring |
| Mild steel | To your drawing | Plain washers, shims, split pins and pressed parts that do not need to spring back |
| Stainless steel | SS 304 | Parts that must resist corrosion |
| Stainless steel | SS 316 | Parts in wet, salty or chemical service |
Finishes: zinc plated with yellow or green trivalent passivation, phosphating, or blackening. Other grades and finishes to your drawing.
Secondary operations
After the press
- Heat treatment: in-house or with outside partners, depending on the volume.
- Finishing: zinc plating with yellow or green trivalent passivation, phosphating and blackening, in-house or with outside partners, depending on the volume.
- Deburring in-house: a vibro finisher, a tumbler and a metal polishing machine.
- Packing: sealed on an automated sealing machine for dispatch.
Request for quotation
Send us the drawing.
We reply with a feasibility note within 2 working days for a part made to a standard, and within 5 working days for a custom part. PDF, DWG and STEP files accepted.
Or email the drawing to inquiry@photoray.co.in.